What does the system consist of?
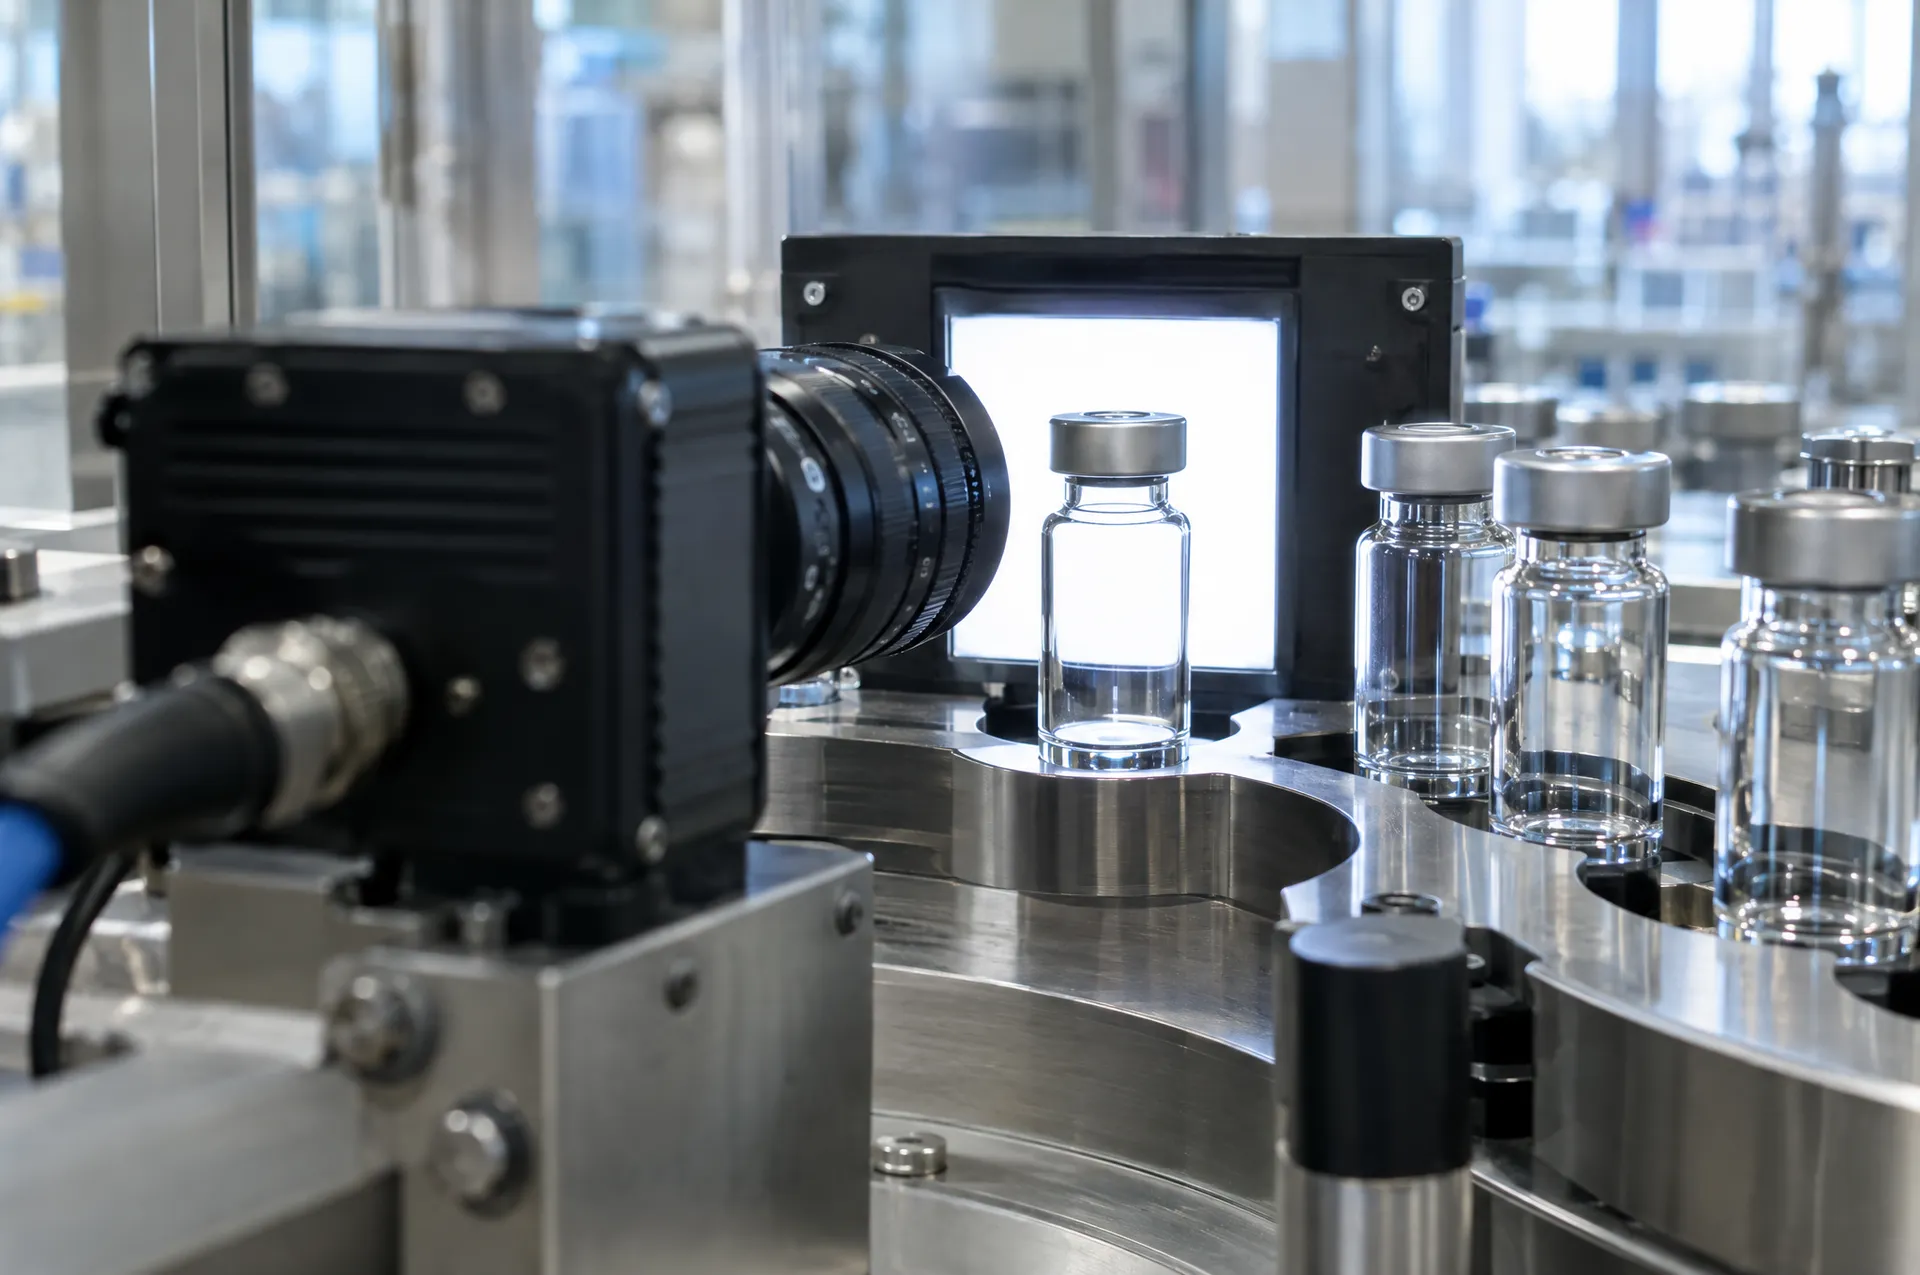
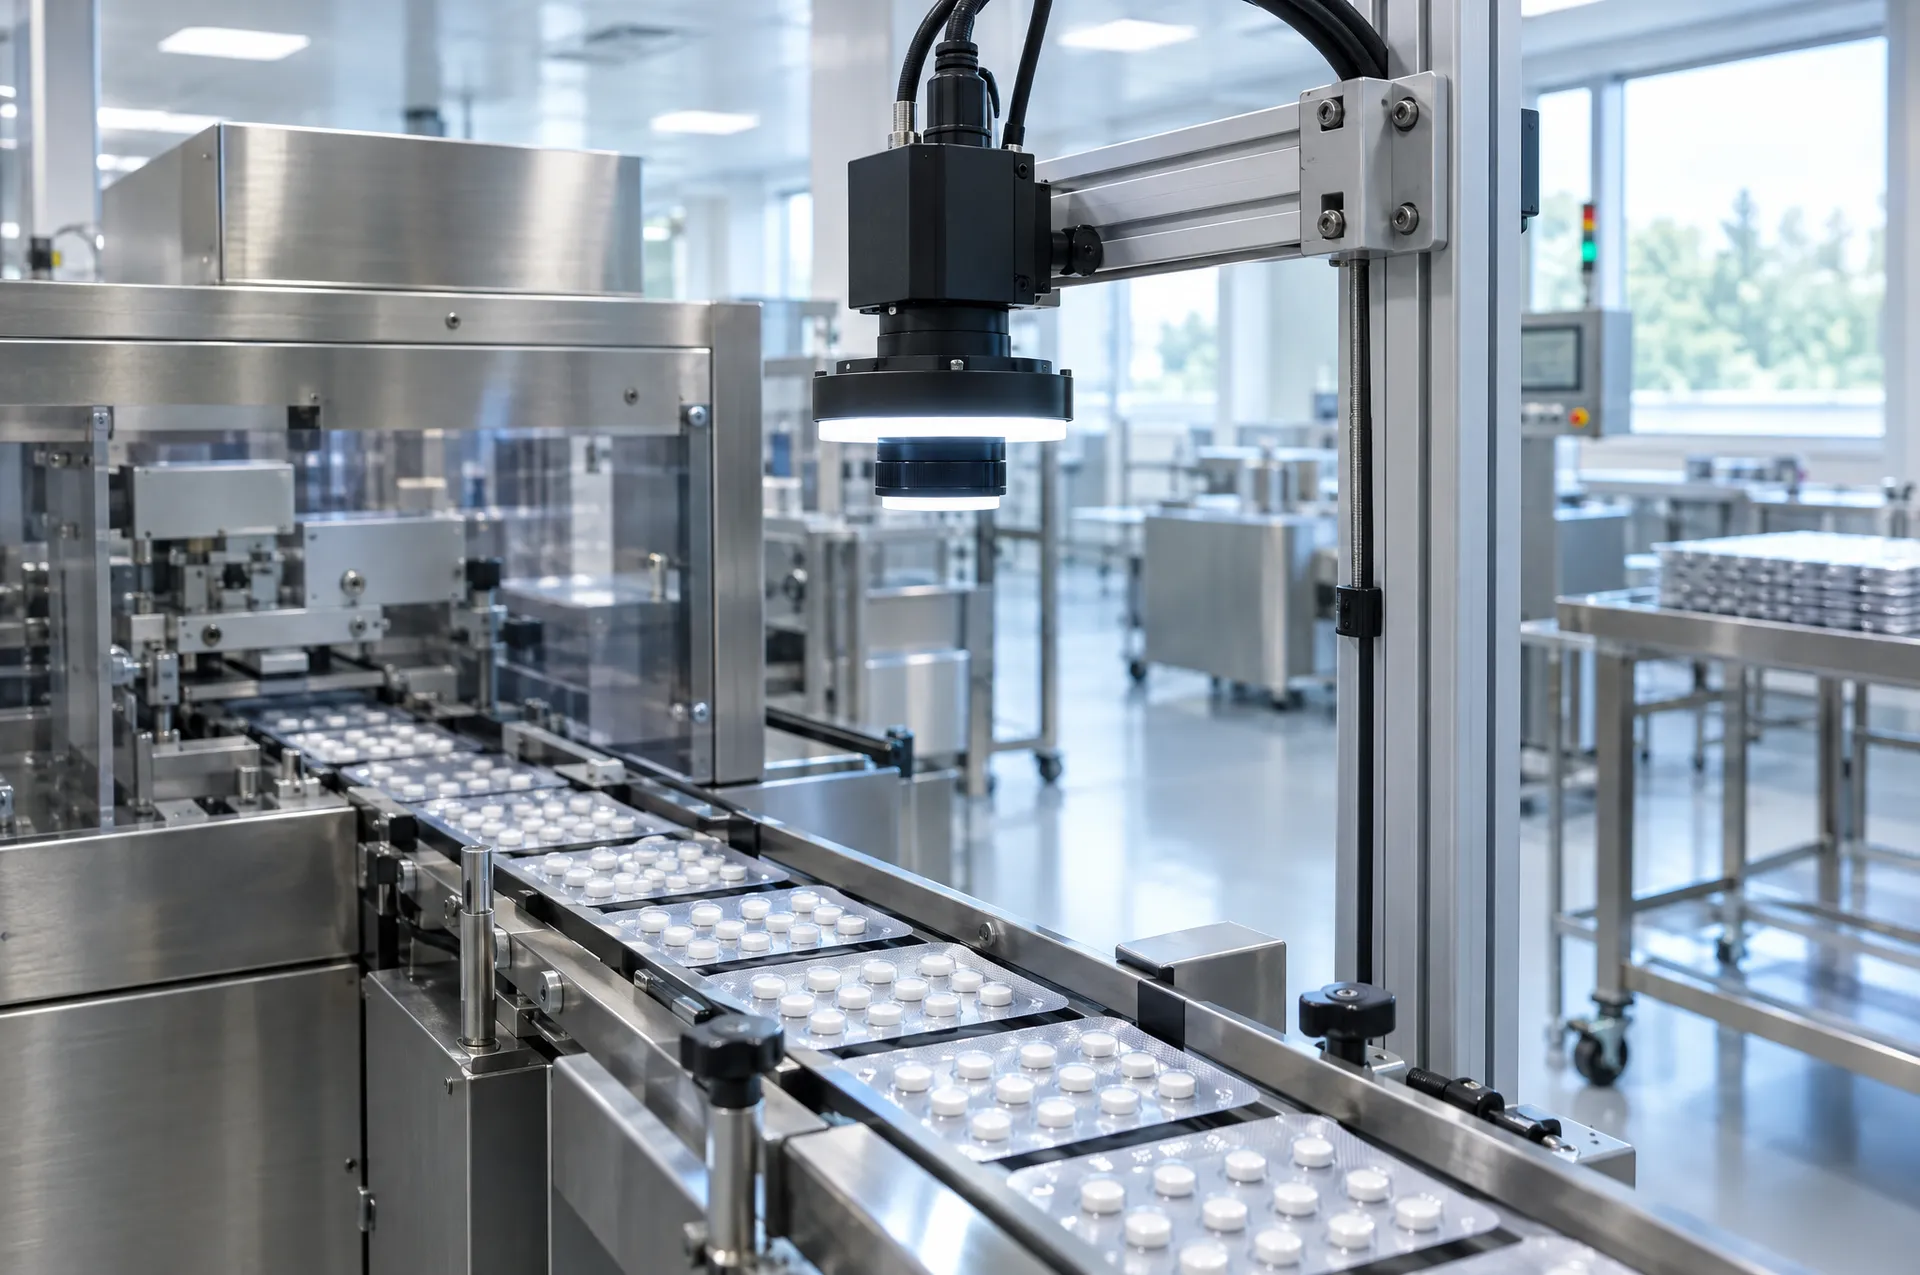
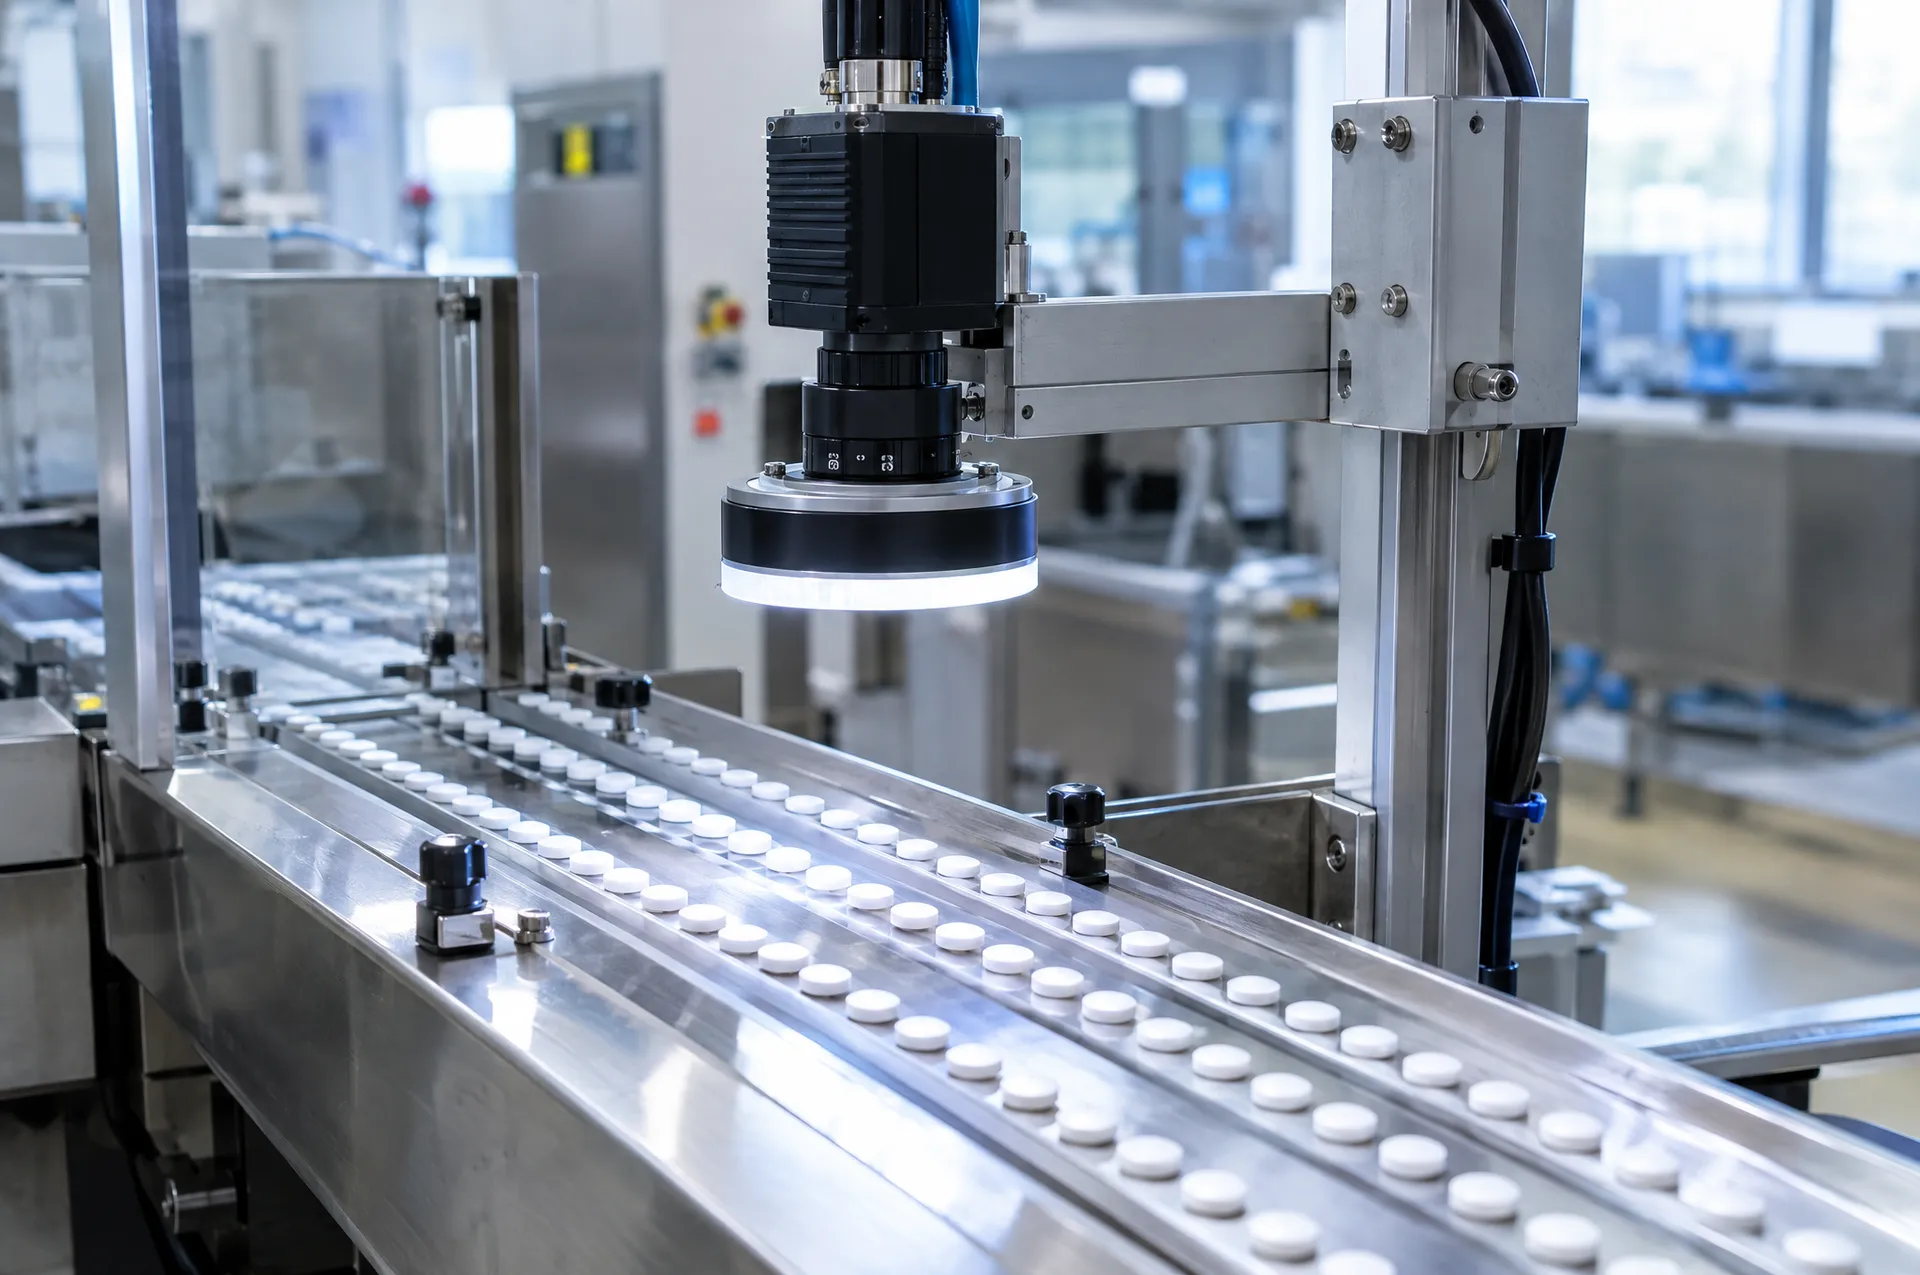
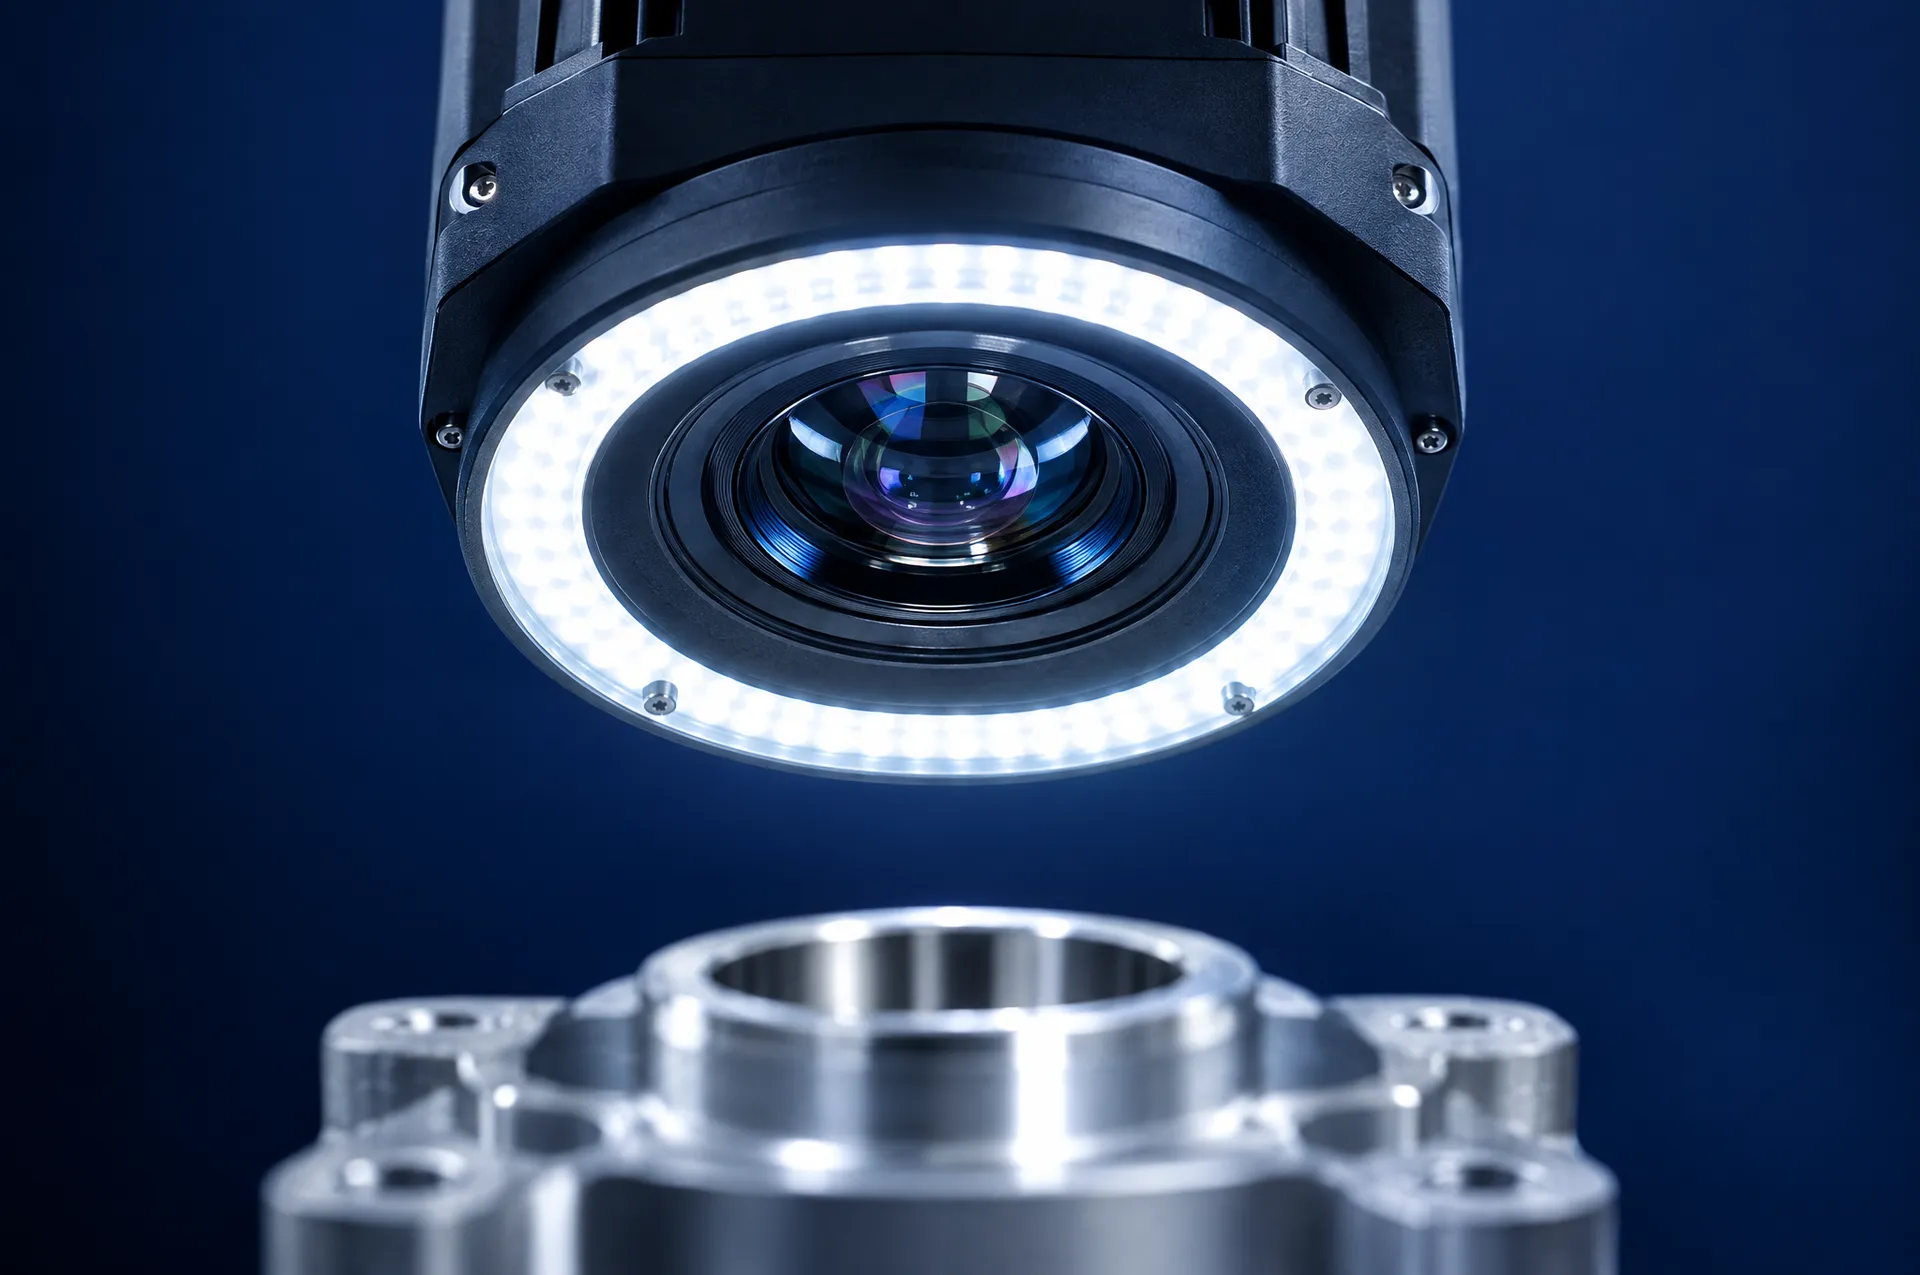
An industrial machine vision system consists of a camera, a lens, lighting, decision software and the line connection. A sensor signals that the product has arrived, the camera captures an image, the software makes the decision and the result is sent to the rejector.
A good result often starts with the image, before the software. If lighting suited to the surface is not chosen, the defect does not appear in the image and no model can find it.
Where is it used in manufacturing?
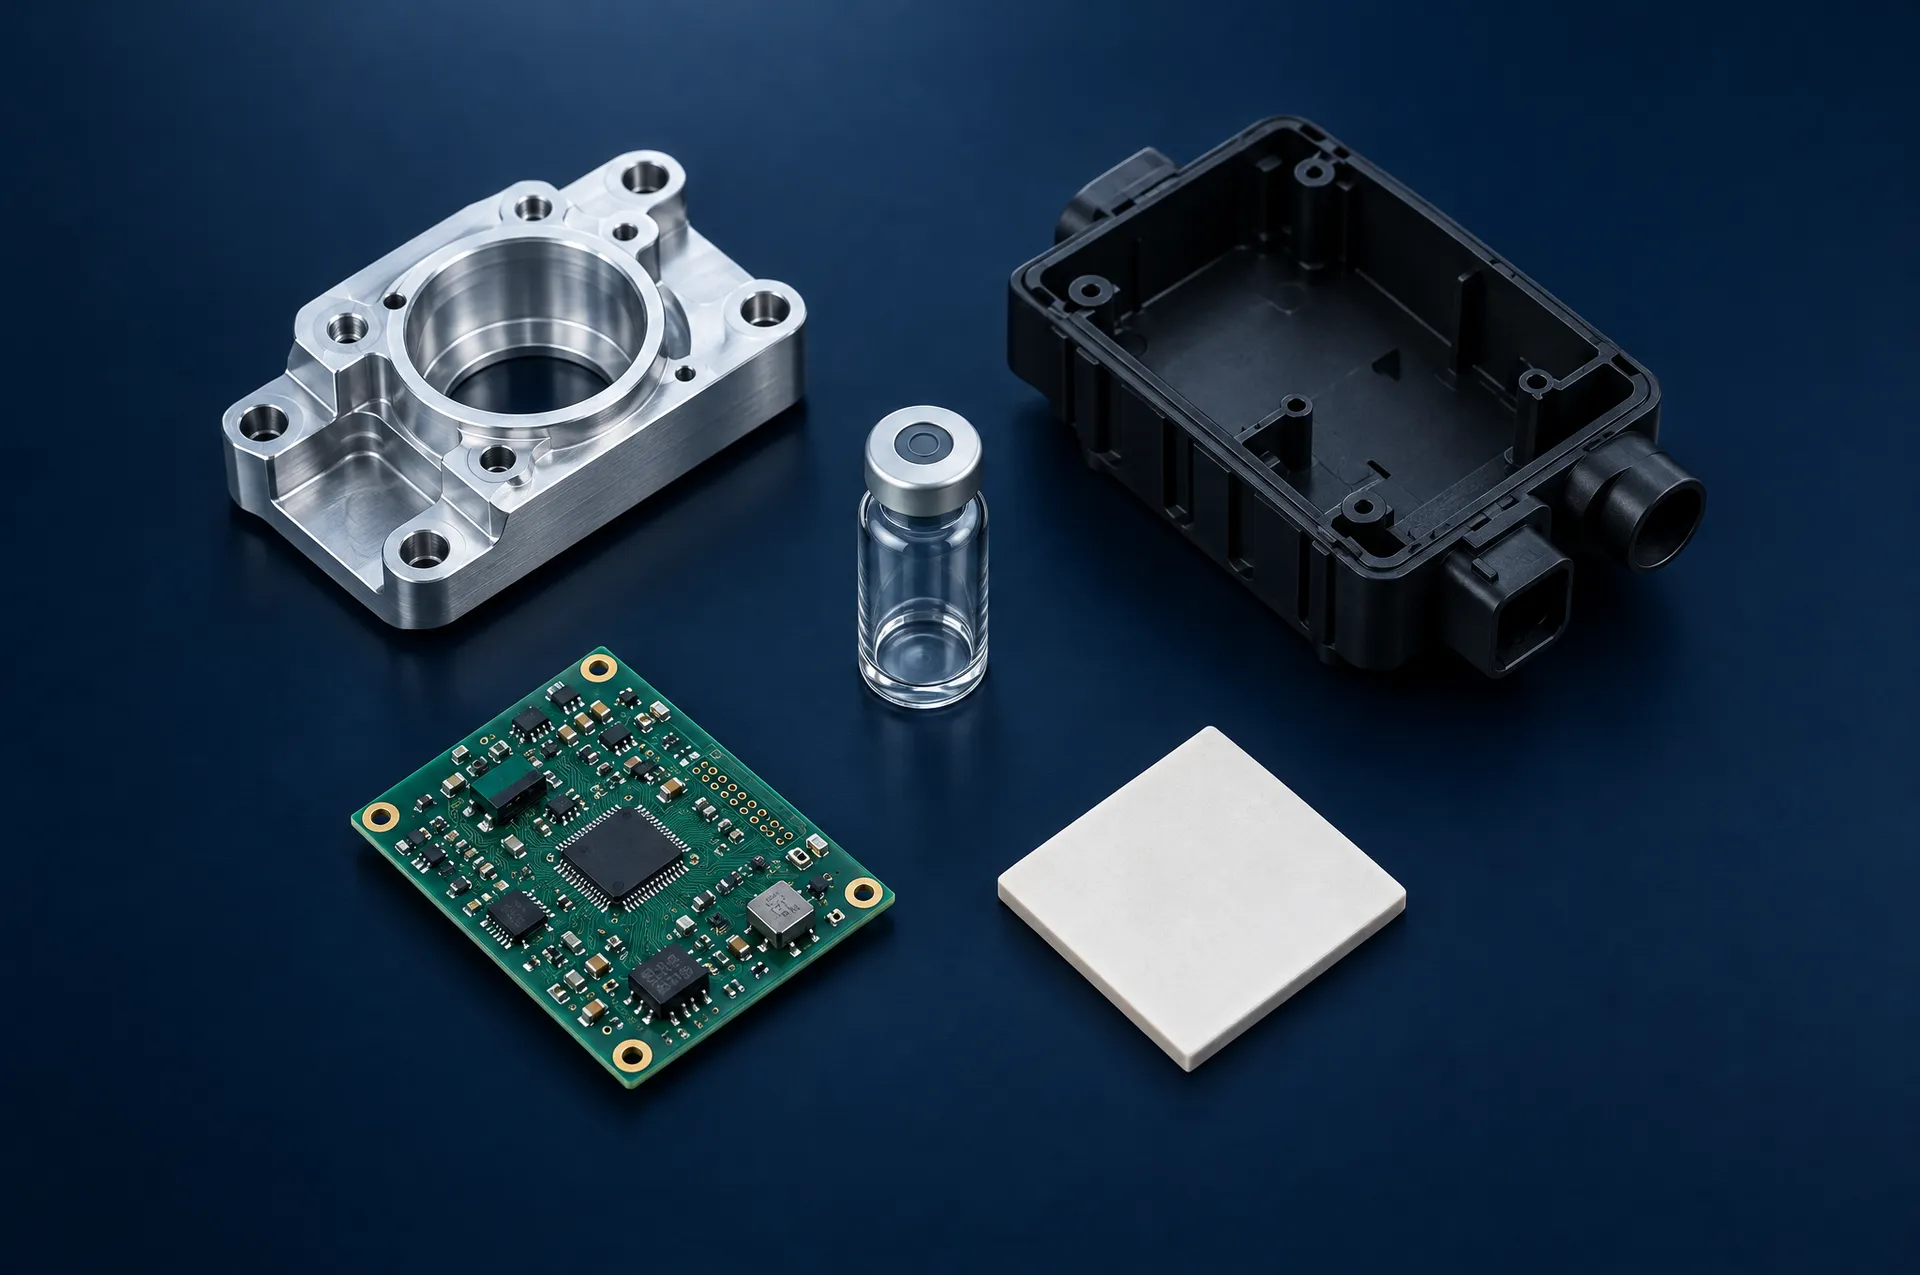
The most common applications are defect detection, surface inspection, assembly and packaging verification, measurement, and counting and sorting. A single station can perform several of these inspections together.
What should be clear before installation?
Which defects need to be caught, the production speed, where the camera will be placed and how defective products will be rejected should be defined in advance. This information directly affects the scope and cost of the system.